 WhatsApp
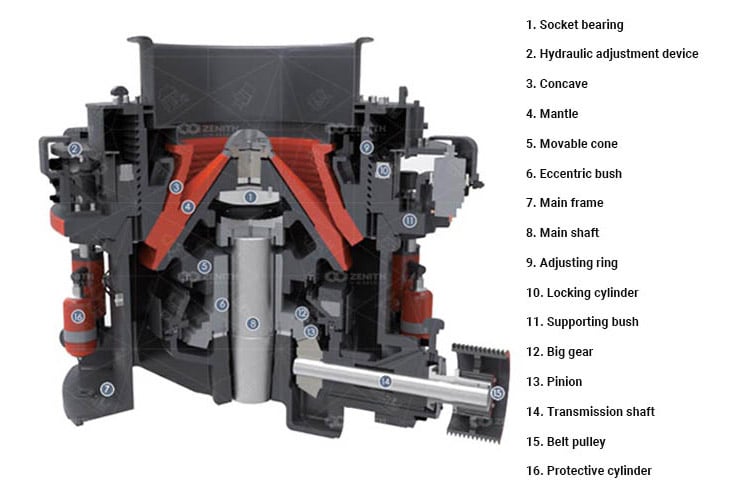
In the high-stakes world of mineral processing, the Cone Crusher is the workhorse of secondary and tertiary crushing. However, the profitability of your entire flowsheet often hinges on two critical components: the Mantle and the Bowl Liner.
Wear parts are not just operational costs; they are the frontline of your production. When these parts wear prematurely, you face a triple threat: increased spare parts expenditure, labor-intensive changeouts, and lost revenue due to unplanned downtime. By implementing professional maintenance strategies, operators can often extend liner life by 20% to 40%, directly impacting the bottom line.
Why Wear Part Lifespan Matters for Your ROI
Every millimeter of manganese steel worn away represents a specific volume of crushed rock. However, uneven or accelerated wear reduces the efficiency of the crushing chamber.
- Minimized Downtime: Fewer changeouts mean more hours of active production.
- Consistent Product Quality: Worn liners struggle to maintain the Closed Side Setting (CSS), leading to "oversize" material and poor grain shape.
- Lower Cost-Per-Ton: Extending lifespan reduces the frequency of capital outlay for new castings.
Consider this: A typical set of cone crusher liners processing hard rock might last 800–1,200 hours. Extending that life by just 20% could save your operation $15,000–$30,000 per year or more, depending on your crusher size and production volume.
Key Factors Affecting Mantle and Bowl Liner Wear
Understanding what drives wear is the first step to controlling it. Three primary factors determine how quickly your liners wear out.
1. Feed Material Characteristics
The material you crush has the single greatest impact on liner wear. Three specific characteristics matter most:
Abrasiveness (Abrasion Index)
- Materials with high silica content (e.g., granite, basalt, river pebbles) are highly abrasive
- High abrasion accelerates wear exponentially
- Action: If you process highly abrasive rock, expect shorter liner life and budget accordingly. Consider upgrading to higher-grade manganese (Mn22% instead of Mn18%).
Hardness (Compressive Strength)
- Harder rock requires more crushing force, increasing liner stress
- Soft rock (limestone, sandstone) causes less wear but may lead to other issues like packing
- Action: Match your liner profile to the material hardness (see cavity selection below).
Moisture and Clay Content
- Wet, sticky material can pack in the crushing chamber, causing uneven pressure and localized wear
- Clay also prevents proper work-hardening of the manganese surface
- Action: Pre-screen or dry material before feeding if moisture exceeds 8-10%.
2. Feeding Method: Choke Feeding vs. Trickle Feeding
The way material enters the crushing chamber directly affects wear patterns, product quality, and liner life.
| Feeding Method | Wear Pattern | Effect on Liner Life |
|---|---|---|
| Choke Feeding (chamber kept full) | Uniform wear across entire liner surface | Extended life (20-30% longer) |
| Trickle Feeding (intermittent or partial fill) | Localized wear on lower portion; uneven wear | Reduced life; risk of premature failure |
| Segregated Feed (material falling to one side) | One-sided wear; bowl tilting | Severely reduced life; potential crusher damage |
Why Choke Feeding Matters:
When the chamber is kept full, interparticle crushing occurs—rock crushing rock. This distributes wear evenly across the liner surface and protects the manganese from direct impact. In contrast, trickle feeding causes direct impact between rock and liner, accelerating wear and creating deep grooves.
Best Practice: Use an automated feeder with level sensors to maintain a consistent, full chamber at all times.
3. Choosing the Right Chamber Profile
Cone crushers offer different cavity profiles (chamber shapes) for specific applications. Using the wrong profile for your material dramatically accelerates wear.
| Cavity Type | Best Application | Why It Matters |
|---|---|---|
| Coarse (Standard) | Primary or secondary crushing of large feed (200-450mm) | Designed for high reduction; wider liners resist impact |
| Medium | All-around secondary crushing | Balance of wear life and reduction |
| Fine (Shorthead) | Tertiary crushing for fine product (under 20mm) | Narrower liners; sensitive to overfeeding |
Common Mistake: Using a fine cavity for coarse material. The narrow chamber forces rock to crush against liners rather than against other rock, causing rapid wear and potential liner cracking.
Best Practice: Match your liner cavity to your feed size and reduction target. When in doubt, consult your crusher manual or supplier.
Best Practices to Maximize Cone Crusher Liner Life
Now that you understand the key factors, here are six proven practices to extend liner life, reduce change-out frequency, and lower your cost per ton.
1. Monitor and Optimize Work-Hardening of Manganese Steel
Manganese steel (Mn13%, Mn18%, Mn22%) is unique: it hardens under impact. When rock strikes the liner surface, the manganese work-hardens, becoming harder and more wear-resistant. However, this requires proper impact force.
- Sufficient impact (choke-fed, hard rock): Work-hardened surface (500-550 BHN); extended life
- Insufficient impact (soft rock, trickle feeding): No work-hardening (220-250 BHN); rapid wear
Best Practice:
- Ensure choke-fed operation to generate sufficient impact energy
- For soft rock applications, consider alternative materials (e.g., high-chrome iron) that do not rely on work-hardening
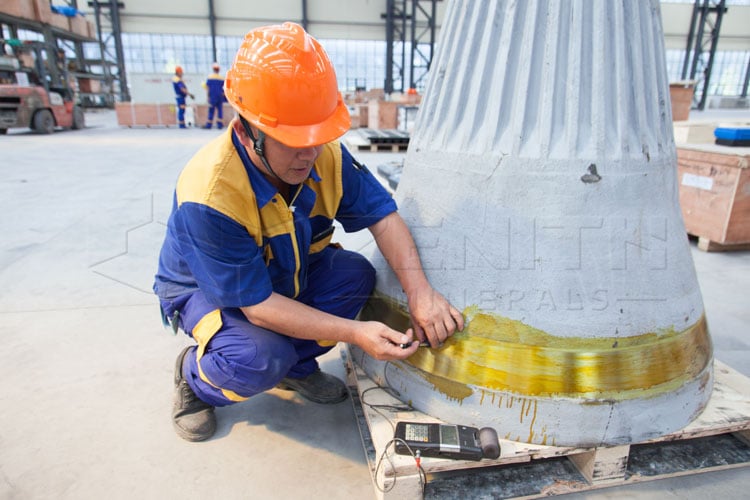
- Use a hardness tester to periodically check surface hardness
2. Ensure Uniform Backing Compound Application
The backing compound (epoxy or polyester resin) fills the gap between the liners and the crusher frame. It transmits crushing forces evenly and supports the liner.
| Poor Application | Consequence |
|---|---|
| Air pockets or voids | Liner flexes under load; cracking; premature failure |
| Incomplete fill | Uneven pressure; localized wear |
| Improper curing | Weak support; liner movement |
Best Practice:
- Follow the manufacturer's mixing and pouring instructions precisely
- Pour backing compound slowly to allow air to escape
- Allow full curing time before putting the crusher back into service
- Inspect used liners after removal—void marks indicate poor application
3. Avoid Tramp Iron and Other Uncrushable Objects
Nothing destroys cone crusher liners faster than tramp iron (bolts, excavator teeth, rail spikes) or other uncrushable material. Even with tramp release systems, each tramp event:
- Grows the liner surface
- May crack the mantle or bowl liner
- Disrupts the work-hardened surface
Best Practice:
- Install a metal detector on the feed conveyor before the crusher
- Use a magnetic separator (especially after primary crushing)
- Train operators to stop the feed immediately if tramp metal is suspected
4. Measure and Record Liner Wear Data
You cannot manage what you do not measure. Track liner wear systematically to predict replacement intervals and identify abnormal wear patterns.
| What to Measure | Frequency | Why |
|---|---|---|
| Liner thickness at 4-6 points | Weekly or monthly | Track wear rate; predict remaining life |
| CSS (Closed Side Setting) | Daily | Monitor for setting drift |
| Power draw trend | Continuous | Spikes indicate liner issues |
| Product particle size | Weekly | Detects chamber wear before failure |
Best Practice: Use a simple spreadsheet to log measurements. Compare actual life to predicted life and adjust maintenance schedules accordingly.
5. Rotate Liners When Possible
On some cone crusher models, liners can be rotated (turned 180 degrees) to extend life. This is particularly effective when wear is uneven.
- Slightly uneven (one side more worn): Evening out wear; extra 15-25% life
- Feed segregation wear: Significant extension
Note: Not all crusher designs allow rotation. Check your manual first.
6. Train Your Operators
The best liners in the world will fail prematurely if operators do not understand proper crusher operation.
| Operator Error | Consequence |
|---|---|
| Starting crusher empty | No material cushion; liners take direct impact |
| Opening CSS too tight | Overload; liner cracking |
| Ignoring power draw spikes | Over-compaction; uneven wear |
| Feeding from only one side | One-sided wear; bowl tilting |
Best Practice:
Conduct regular operator training on:
- The importance of choke feeding
- Reading and responding to power draw
- Proper CSS setting procedures
- Recognizing signs of liner wear
Liner Material Selection—Mn18% vs. Mn22% vs. Alternatives
Choosing the correct manganese grade is essential for maximizing liner life in your specific application.
| Material | Best Application | Characteristics |
|---|---|---|
| Mn14% | Soft, non-abrasive rock (limestone, gypsum) | Lower cost; limited work-hardening |
| Mn18% (Standard) | General purpose; most medium-hard to hard rock | Best balance of life and cost; works for 80% of applications |
| Mn22% (High Manganese) | Extremely hard, highly abrasive rock (granite, basalt, iron ore) | Higher initial cost; superior work-hardening (550+ BHN); 20-30% longer life than Mn18% |
| High-Chrome Iron | Low-impact applications (soft rock, fine crushing where impact is minimal) | Excellent abrasion resistance; does not require impact to harden |
Selection Guide:
- For most quarries (limestone, river gravel): Mn18% is sufficient
- For hard rock, high-abrasion (granite, basalt): Upgrade to Mn22%
- For extremely abrasive conditions (iron ore, quartzite): Consider special alloys or shorter change intervals
FAQ – Questions from Real Buyers
Q1: When should I replace my cone crusher liners, and how can I predict the timeframe?
A: There is no universal "one-size-fits-all" timeframe because wear life depends entirely on your material's abrasiveness. However, you can manage this through two methods:
Predictive Planning: For most operations, liners are replaced once they reach 10% to 15% of their original weight. We recommend tracking the total tonnage processed to create a historical wear-rate benchmark for your site.
Field Indicators: It is time for an immediate change if you encounter any of the following:
- Adjustment Limit: You have reached the mechanical limit of the crusher and can no longer maintain the required CSS.
- Thickness: The liner has worn down to approximately 19mm–25mm at the thinnest point.
- Capacity Drop: A noticeable surge in power consumption or a significant drop in TPH (tons per hour).
Q2: Why are my liners wearing unevenly?
A: This is usually caused by "segregated feeding," where large rocks fall to one side of the hopper and fines to the other. This creates uneven pressure, causing one side of the mantle to wear significantly faster than the other.
Q3: Can I weld or build up worn liners to extend their life?
A: In short: No. Manganese steel is a work-hardening alloy. The intense heat from welding can change the metallurgical structure of the casting, making it brittle and prone to catastrophic cracking under crushing loads. Furthermore, build-up welding can cause the liner to lose its precise fit, potentially damaging the crusher's head or bowl seat. It is always safer and more cost-effective to replace the liner.
ZENITH – Your Partner in Crushing Efficiency and Lower Cost-Per-Ton
Extending the life of your cone crusher mantle and bowl liner is not luck—it is a systematic process of proper selection, operation, and maintenance.
By implementing the practices outlined in this guide—choke feeding, correct cavity selection, feed distribution, data tracking, and operator training—you can realistically extend liner life by 15-30%, saving tens of thousands of dollars annually.
Need Reliable Cone Crusher Wear Parts?
At ZENITH, we offer high-precision manganese liners (Mn14%, Mn18%, Mn22%) manufactured to exact OEM specifications. Our wear parts feature:
- Precision casting with X-ray quality inspection
- Dimensional tolerance within 2mm
- Extended life through optimized metallurgy
- Competitive pricing with global delivery
Contact our team today for:
- A free liner life assessment
- Customized wear part recommendations based on your material
- A quotation for Mn18% or Mn22% mantle and bowl liner sets

 24/7 Online